Precise liquid level control with quality guarantee
In today's industry, precise liquid level monitoring is an absolute necessity. From the food industry to the chemical and pharmaceutical industries, every sector requires solutions that ensure reliability, safety, and complete control over production processes. SENOTEC, a renowned German manufacturer, has been providing top-quality liquid level sensors and amplifiers for years, successfully used in the most demanding applications.
As the official and exclusive distributor SENOTEC in Poland, Central Europe, and the Baltic States, ProTech not only offers access to the brand's full range of products but also provides professional advice, technical support, and fast delivery. In this article, we'll explain why you should trust SENOTEC solutions and why ProTech is the partner you should choose.
Who is SENOTEC and what does it offer?
The history and specialization of the German manufacturer
SENOTEC GmbH was founded in Germany and has focused on developing innovative technologies for precise liquid level measurement since its inception. For years, it has been a pioneer in liquid level detection based on optical and capacitive technologies, making it one of the most trusted manufacturers in the industrial automation industry.
SENOTEC products are designed with the highest quality and long-term reliability in mind. Their devices are used in applications where even the slightest inaccuracy can lead to significant losses or hazards. Therefore, their sensors and amplifiers meet stringent quality and safety standards, such as ISO 9001, ATEX, and FDA for the food industry.
Global presence and distribution partners
SENOTEC is a global brand – its equipment is installed in hundreds of factories worldwide, including leaders such as Homag, IMA, Duspohl, SCM, Biesse, Valco Meltron, Felder KG, Kolbus, Robatech AG, Barberan SA, SM-Klebetechnik, and Wohlenberg. The company's international presence is based on a network of trusted partners, such as ProTech, which is responsible for distribution and customer support in Poland, Central Europe, and the Baltic States.
The official website of the manufacturer Senotec contains detailed technical information, documentation, and new products. ProTech maintains close cooperation with SENOTECheadquarters, ensuring customers receive the latest solutions and quick access to components.
ProTech – Official distributor SENOTEC in Poland and Central Europe
Why is it worth buying SENOTEC products from us?
As an authorized distributor, ProTech offers not only sales of SENOTECdevices but also full technical support, design consulting, and training in sensor installation and use. Thanks to direct contact with the manufacturer, we are able to quickly respond to our customers' needs – from fast deliveries to service support.
When you buy from an official distributor, you can be sure that:
- originality of products and manufacturer's warranty,
- the latest versions of devices and software,
- professional support at every stage of implementation,
- attractive prices and availability from stock.
Additionally, we offer direct access to the full offer:
Markets served: Poland, Baltic countries, Central Europe
ProTech operates not only in Poland. Our services are also available to clients from Lithuania, Latvia, Estonia, the Czech Republic, Slovakia, Hungary, and other Central European countries. Our experience in working with international clients allows us to effectively address the needs of diverse markets and industries.
Application of SENOTEC sensors – Where are they irreplaceable?
Food industry
In food production, cleanliness, precision, and safety are paramount. SENOTEC sensors meet stringent hygiene standards (e.g., FDA, EHEDG), and their design allows for safe installation in milk, juice, or sauce containers without the risk of product contamination. Contactless liquid detection eliminates the risk of false readings and minimizes maintenance time.
Chemical and pharmaceutical industry
In these sectors, SENOTEC sensors are used to measure the level of aggressive and hazardous liquids—from acids to industrial alcohols. Their chemical resistance, tightness, and safety certifications (including ATEX) make them ideal for use in harsh environments.
OEM Applications and Industrial Automation
SENOTEC sensors can be easily integrated with industrial automation systems, PLCs, and SCADA systems. The manufacturer offers a variety of interfaces (PNP/NPN, relay outputs, analog), making them suitable for any system architecture. In OEM applications, they are used in CIP/SIPcleaning equipment, dosing stations, mixers, and many others.
Wood and furniture industry
Global leaders such as Homag, SCM, Biesse, and Felder KG use SENOTEC sensors in their woodworking and furniture production lines. The sensors monitor fluid levels in lubrication systems, coolant circulation systems, and adhesive dispensing systems, ensuring operational continuity and quality repeatability.
Packaging and printing industry
Companies such as IMA, Kolbus, and Wohlenberg supply packaging, printing, and bookbinding machines where SENOTEC sensors monitor glue, varnish, and ink levels. Stable media detection reduces downtime and ensures consistent product quality—from food packaging to high-end publications.
Adhesive Industry and Coating Technology
Robatech AG, Valco Meltron, SM-Klebetechnik, and Barberan SA specialize in adhesive dispensing systems and surface coating technologies. In these applications, SENOTEC sensors monitor the levels of resins, adhesives, and coatings in processing tanks, enabling precise, cost-effective dispensing and uninterrupted production.
Specialized machinery industry
Manufacturers such as Duspohl (profile wrapping machines) use SENOTEC sensors to monitor the levels of hot melt adhesives, oils, and other process media. The sensors maintain reliability under varying temperatures, viscosities, and pressures, which is crucial in demanding operating conditions.
SENOTEC Sensors – What makes them stand out?
Operation technology and high measurement precision
One of the greatest advantages of SENOTEC sensors is their exceptional measurement accuracy, which allows for effective liquid level detection even in the most challenging conditions. The manufacturer uses advanced optical and capacitive technologies that not only eliminate errors resulting from external conditions but also enable the detection of liquids with various properties – from water and oils to chemicals and viscous mixtures.
SENOTEC optical sensors are renowned for their lack of moving parts, which translates into their reliability. Unlike conventional floats or radar probes, they are not susceptible to mechanical wear or sediment. Furthermore, this technology enables lightning-fast sensor response—even in milliseconds—which is invaluable in the automation of production processes.
The high temperature and pressure resistance of the devices is also important - many models operate in the temperature range from -20°C to +130°C, as well as under pressure up to 10 bar, which allows them to be used in pressurized tanks and CIP/SIPsystems.
Compatibility and assembly flexibility
Engineers and integrators value SENOTEC not only for its quality but also for its ease of installation and integration into existing systems. Sensors are available in a variety of thread sizes (e.g., G1/2″, G3/4″, M12), cable lengths, and power and signal output options. This makes them ideal for both retrofitting existing installations and new projects.
The manufacturer also offers plug-and-play sensors that require no calibration – they are ready to use after installation and connection, significantly speeding up the implementation process. For more advanced applications, models are available that can be configured via an amplifier or communication interface.
Example models and their parameters
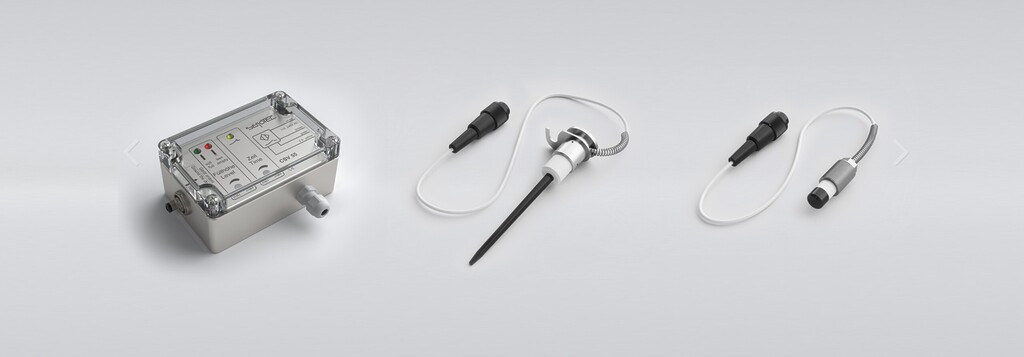
The most popular SENOTEC sensor models include:
- optical sensor for detecting liquid levels in stainless steel tanks, resistant to high temperatures.
- miniature liquid level sensor for OEM systems, with lightning-fast response time.
- capacitive sensor for detecting conductive and non-conductive liquids, ideal for harsh environments.
The full range of models can be found at:
👉 SENOTEC sensors – full offer
SENOTEC Amplifiers – An Essential Complement to Sensors
How do amplifiers work?
SENOTEC amplifiers are a key element of liquid level detection systems – they are responsible for interpreting the sensor signal and transmitting it, for example, to a PLC or automation system. This allows for the precise determination of whether a given tank contains liquid and its quantity.
The amplifier works by amplifying the sensor's output signal and adapting it to the requirements of the host system. It also allows for sensitivity calibration, switching point setting, and operating mode selection (e.g., "NO"/"NC").
Overview of available models
SENOTEC offers several amplifier models tailored to various application needs:
- basic amplifier for one sensor, mounted on a DIN rail, with sensitivity adjustment.
- amplifier with two input channels, allowing control of two sensors simultaneously.
- advanced amplifier with auto-calibration function and pulse operation mode, ideal for dynamic applications.
All models are compatible with SENOTECsensors, eliminating the risk of integration problems and ensuring the highest reading quality.
Details can be found here:
👉 SENOTEC Amplifiers – see products
Integration with control systems
The advantage of SENOTEC amplifiers is their full compatibility with industrial automation systems from Siemens, Mitsubishi, Schneider, and Omron. They support both standard digital and analog signals (0-10V, 4-20mA) and are suitable for installation in control cabinets.
This means that they are used not only in classic production lines, but also in advanced SCADA systems where quick reactions and accuracy are required.
Benefits of implementing SENOTECsolutions
Process optimization
The use of SENOTEC sensors and amplifiers leads to real optimization of production processes. Precise liquid level measurement allows for automated filling, dosing, and emptying of tanks, preventing overflows or material shortages in the process.
Reduction of downtime and losses
One of the main causes of downtime in production lines is incorrect liquid level detection. With SENOTEC this risk is virtually eliminated – the devices are immune to interference, insensitive to foam or sediment, and operate reliably even in conditions of high dust, vibration, and fluctuating temperatures.
Safety and compliance
SENOTEC sensors meet the most important safety and quality standards, both European and international. ATEX versions allow for operation in potentially explosive atmospheres, and food-grade models are FDA certified. This makes them the number one choice for companies concerned about regulatory compliance and personnel safety.
SENOTEC sensors – full offer
If you're looking for reliable liquid level sensors that ensure accurate measurements in all conditions – from simple applications to industrial automation systems – be sure to check out our full range of SENOTECsensors. You'll find models including:
- optical for transparent and turbid liquids,
- capacitive for conductive and non-conductive substances,
- compact solutions for OEMs.
Each product is described in detail, including technical documentation, installation instructions, and application suggestions. If you need help selecting a model, our technical advisors are available.
SENOTEC Amplifiers – see products
We also offer a wide range of SENOTECamplifiers, perfectly matched to their sensors. Whether you're looking for a simple signal amplifier or a sophisticated system with auto-calibration, you'll find the right model in this category.
On each product page you will find:
- technical data and connection diagrams,
- examples of applications,
- comparison of features between models,
- availability and delivery time.
By integrating our online offer with our warehouse, you can immediately check product availability and order them directly through the online store.
SENOTEC in practice – Examples of implementations and successes
Dairy Industry Case Study
One of our dairy clients was struggling with issues related to incorrect milk level measurement in production tanks. Frequent false readings resulted in tank overflows, downtime, and product loss. After analyzing the process, we proposed using SENOTEC optical sensors with dedicated amplifiers.
Implementation effects:
- 100% elimination of tank overflows,
- 20% reduction in filling time thanks to the quick response of sensors,
- reduction of costs related to cleaning and material losses.
Thanks to the use of SENOTECcomponents, the company was able to switch to a fully automated tank filling process, which contributed to a significant increase in efficiency.
Application in the chemical industry
Another successful implementation was the installation of CLS sensors at a cleaning product manufacturing facility. The client required reliable level detection of aggressive liquids (acids, bases) while also maintaining compliance with ATEX standards in potentially explosive atmospheres.
SENOTECsolution:
- capacitive CLS sensors with stainless steel housing,
- amplifiers mounted in the control cabinet,
- full integration with the SCADA system and remote diagnostics.
The result? Trouble-free operation for two years, increased safety, and full compliance with the industrial inspection audit.
Frequently Asked Questions (FAQ)
1. Are SENOTEC sensors suitable for viscous and dense liquids?
Yes, many models are designed for difficult-to-detect liquids, including viscous or foamy ones. SENOTEC optical sensors are insensitive to foam, giving them a competitive advantage.
2. Can SENOTEC sensors be used in ATEX zones?
Yes – the manufacturer offers ATEX-certified models that can be used in potentially explosive atmospheres (e.g. chemical and pharmaceutical industries).
3. What interfaces do SENOTECamplifiers support?
The amplifiers support both digital and analog signals (0-10V, 4-20mA). They can be easily integrated with popular PLCs.
4. Are SENOTEC products immediately available?
ProTech maintains a local warehouse, so many sensor and amplifier models are available immediately or with short lead times.
5. How to choose the right sensor for your application?
Simply contact our technical team. We'll select the perfect solution based on several parameters (fluid type, temperature, pressure, installation method).
Summary – Why choose SENOTEC and PL-ProTech?
Choosing SENOTEC sensors and amplifiers guarantees the highest quality, precision, and reliability. These products are manufactured in Germany, meet the most stringent industry standards, and have been used in thousands of industrial applications worldwide for years. By partnering with ProTech, you can be sure to receive not only the product but also comprehensive technical support, fast delivery, and access to the latest technologies.
Need help choosing or a quote?
We'll help you choose the right part or solution for your machine. Call or write to us — we advise based on real hands-on maintenance experience.